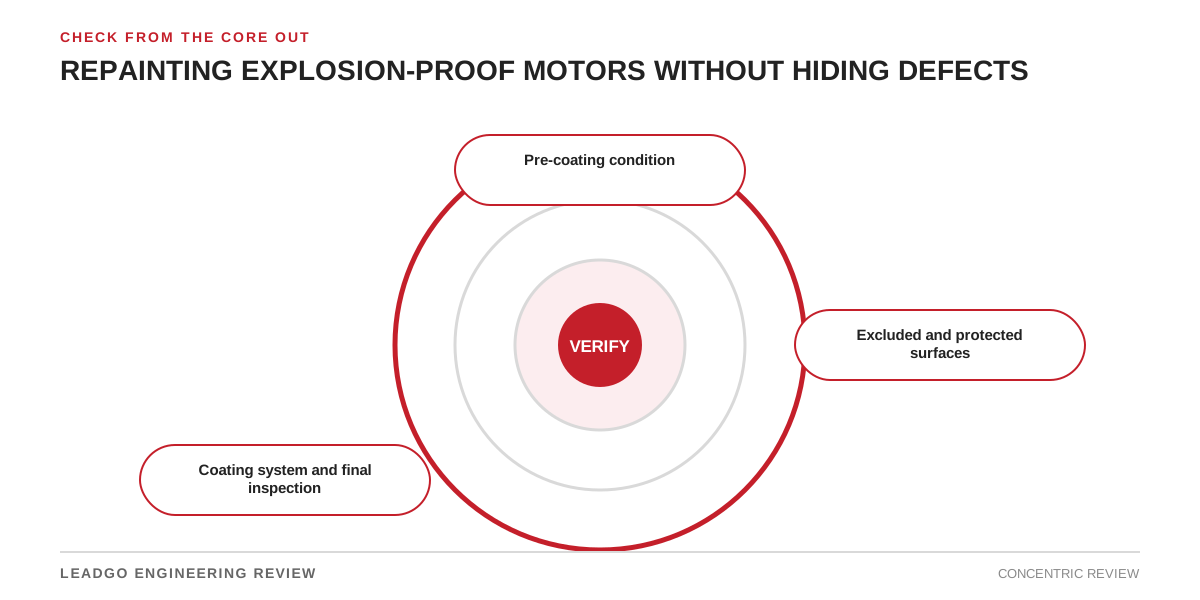
Repainting can extend external corrosion protection, but it cannot repair lost metal, damaged threads or compromised explosion-protection joints. Record the pre-cleaning condition first.
| Surface | Action | Final evidence |
|---|---|---|
| External cast/steel surface | Prepare and coat to approved system | Preparation and dry-film records |
| Nameplate and Ex marking | Mask and preserve | Legibility photograph |
| Flamepath or machined joint | Protect from blasting and coating | Clean condition inspection |
| Earth contact, drain and entry | Mask/keep functional | Continuity and visual check |
Approve the scope before preparation
Identify chemicals, salt, UV, washdown and expected service life. Select preparation and coating compatible with the substrate and existing system. Aggressive blasting near joints, seals or windings needs controlled exclusion and containment.
Stop if cleaning exposes deep pitting, cracks, distorted covers, damaged threads or uncertain prior repair. These need a technical disposition before coating resumes.
After cure, remove masking without damaging edges. Confirm no paint bridges joints, blocks drains, fouls the fan or obscures fasteners and warning labels. Retain product batch, colour, preparation grade, thickness readings, photographs and inspector approval.
Related reading: Ex motor maintenance inspection and coastal motor specification.